If you’ve ever worked with injection molded parts, you know that thin-walled components—think medical device housings, consumer electronics casings, or automotive connectors—are in high demand right now. As an injection molded parts supplier with 12 years on the shop floor, I hear customers tell me they want thinner walls to cut material costs, reduce product weight, and shrink overall part size. But here’s what most folks don’t tell you: producing thin-walled injection molded parts isn’t just tweaking a mold or machine setting. It’s a delicate balance of material science, mold design precision, and real-time process control that trips up even experienced teams. Let me walk you through the biggest challenges we face, straight from the press room. Injection Molded Parts
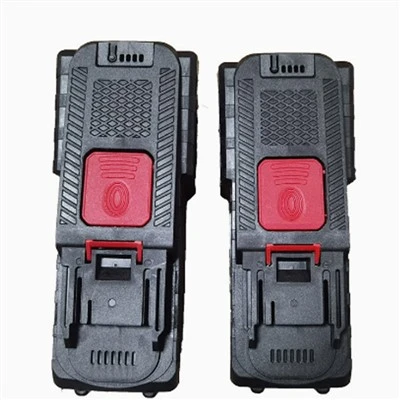
First, there’s the obvious one: flow length vs. wall thickness. Thin walls mean the molten plastic has to travel farther through the mold’s cavities without cooling too fast. To put this in numbers, a standard thick-walled part (say, 3mm) might have a flow length of 150mm, but a thin-walled part (1mm or less) could need that same flow length—sometimes even longer, especially for parts with complex features like undercuts or fine mesh patterns. When the plastic cools, it solidifies from the walls inward. If it moves too slow through a thin section, the leading edge of the melt freezes before it fills the entire cavity. That’s a short shot, and it’s not just a waste of material; it can derail a production run that’s already scheduled to meet a customer’s deadline. We once had a client in the medical industry who needed 0.8mm wall parts for a fluid filter housing. We tried a standard PP resin, and the melt froze halfway through the 200mm flow path. We had to switch to a low-viscosity medical-grade resin—something that flows easier without compromising biocompatibility—but that added a 15% material cost. The client had to adjust their budget, which is a conversation no one wants to have.
Next, part warpage is a silent killer here. Thin walls are more flexible, so uneven shrinkage during cooling can twist, bend, or curve the part even after it’s ejected. Shrinkage happens because plastic molecules align as they flow, and different areas of the part cool at different rates. For example, a thin-walled part with a thick rib (used for structural support) will shrink more around the rib than the thin wall. That mismatch creates stress, and since the wall is so thin, there’s not enough material to resist the warping. We saw this last year with a consumer electronics client making a 0.7mm thick smartphone bracket. The initial parts came out warped by 2 degrees, which made them unfit for assembly into the phone frame. We fixed it by modifying the mold’s cooling lines to ensure uniform temperature across the cavity, but that required adding 6 precision cooling channels—something we didn’t have in the original mold. Rerouting the cooling system added 2 weeks to the mold build time and an extra $8,000 in tooling costs. The client ended up paying for half of that, which pushed their product launch back by a month. Warpage isn’t just an aesthetic issue; if the part doesn’t fit into the final assembly, it’s useless.
Then there’s tooling precision and mold maintenance, which is way more critical for thin walls. A mold for a thick-walled part can have slight gaps or wear in the cavity walls and still produce a good part. But a thin-walled part’s wall thickness is often held to a tolerance of ±0.05mm—less than the thickness of a human hair. If the mold’s cavity is worn by even 0.02mm, you end up with a part that’s too thin in some areas, which can cause structural failure, or too thick, which leads to material waste and warpage. We run 24/7 for some clients, and mold wear is a constant battle. Last quarter, one of our molds for a 0.6mm thick automotive sensor housing developed a tiny wear spot after 50,000 shots. The parts coming out had walls that varied by 0.1mm, so we had to pull the mold offline, machine a new insert, and re-polish the cavity. That cost $3,500 and a full shift of lost production time. For clients with high-volume orders (we’re talking millions of parts), even minor mold wear can lead to thousands of defective parts before you catch it. Also, thin walls mean mold vents have to be exactly the right size. If vents are too big, flash—excess plastic that oozes out—forms on the part’s edges. If they’re too small, air gets trapped in the cavity, leaving voids that weaken the part. We spend extra time calibrating vent sizes for thin-wall molds, and we check every vent with a micrometer before running production. It’s tedious, but it’s necessary.
Material selection is another challenge that’s easy to overlook. Not all plastics work for thin walls. High-viscosity resins, like some engineering thermoplastics, don’t flow well in thin sections, so they’re often out of the question. That leaves customers with limited options, especially if they need specific properties: UV resistance, impact strength, flame retardancy, or biocompatibility. For example, a client making outdoor lighting housings needed thin walls (0.9mm) with UV stability and impact resistance. We initially suggested a glass-filled ABS, but the glass fibers made the resin too stiff and hard to flow through the thin walls. We switched to a modified polycarbonate blend with 10% fiber, which flowed better, but the fiber content meant the part had a rougher surface finish—something the client didn’t want. We had to adjust the mold’s polish to a higher grade, which added time to the mold build. Even small material changes can ripple through the entire process, from tooling to part quality. And if a customer doesn’t specify the right material upfront, you end up with parts that don’t meet their requirements after they’re made.
Cycle time is a final, often underdiscussed challenge. Thin walls cool faster, so you might think you can run parts faster. But in reality, you can’t—if you do, the part will eject too early, when it’s still soft, and warp or break. We’ve had clients ask us to reduce cycle time from 15 seconds to 10 seconds for a thin-walled component, but when we tested it, 30% of the parts had cracks along the edges where the wall is thinnest. The plastic isn’t fully rigid yet when it’s ejected, so even a small amount of force from the ejector pins can cause damage. We have to adjust the cooling time to make sure the part is fully rigid before ejection, which means cycle times are often 20-30% longer than they would be for a similar thick-walled part. For high-volume orders, that adds up. If you’re making 10 million parts a year, a 5-second extra cycle time means 1.3 million more cycles, more machine hours, and higher energy costs. We have to pass some of that cost on to customers, but we also work with them to optimize the cycle by using faster-cooling resins or modifying the ejector system to use more pins, which distribute the force evenly.
Now, you might be thinking, “So why bother with thin-walled parts at all?” The answer is clear: customers want lighter, cheaper, more compact products, and thin walls are the way to get there. But as a supplier, we don’t just push thin-wall production—we make sure it’s done right. That means investing in precision tooling, real-time process monitoring (we use pressure sensors in the mold to track melt flow and detect short shots early), and close collaboration with customers from the design stage. If you’re a product designer or engineer considering thin-walled injection molded parts, don’t just focus on the wall thickness. Talk to us early in the process, before you finalize the design. We can help you choose the right resin, adjust the mold for uniform cooling, and avoid the common pitfalls that lead to delays or defective parts.
At the end of the day, producing thin-walled injection molded parts is a mix of art and science. It’s not just about running a machine—it’s about understanding how plastic flows, how it cools, and how to make every part meet the exact specs you need. If you’re working on a project that needs thin-walled components, we’re here to help. We can walk you through the challenges we’ve faced, share solutions that have worked for other clients, and make sure your parts are produced to the highest quality standards. Reach out to our team to start a conversation about your next injection molded part project—let’s turn your design into a successful, cost-effective product.
Plastic Household Items References:
- Rosato, D. V., & Rosato, M. G. (2012). Injection Molding Handbook (5th ed.). Hanser Publications.
- Toyota Technical Institute. (2018). Thin-Wall Injection Molding: Process Optimization and Quality Control. Journal of Manufacturing Engineering, 14(3), 45-52.
- American Society of Mechanical Engineers (ASME). (2020). Design Guidelines for Injection Molded Thin-Wall Components. ASME B46.1-2020.
- Engineering Materials Handbook. (2019). Thermoplastics for Injection Molding: Flow and Shrinkage Properties. ASM International.
Yongkang Shunjiang Plastic Products Co., Ltd.
As one of the most professional injection molded parts manufacturers and suppliers in China, we offer a wide range of products with superior quality. Please feel free to wholesale bulk customized injection molded parts from our factory. Also, pricelist is available.
Address: Kangzhuang Road, Xicheng Subdistrict, Yongkang City, Zhejiang Province, China
E-mail: 15158911623@163.com
WebSite: https://www.shunjiangplas.com/
